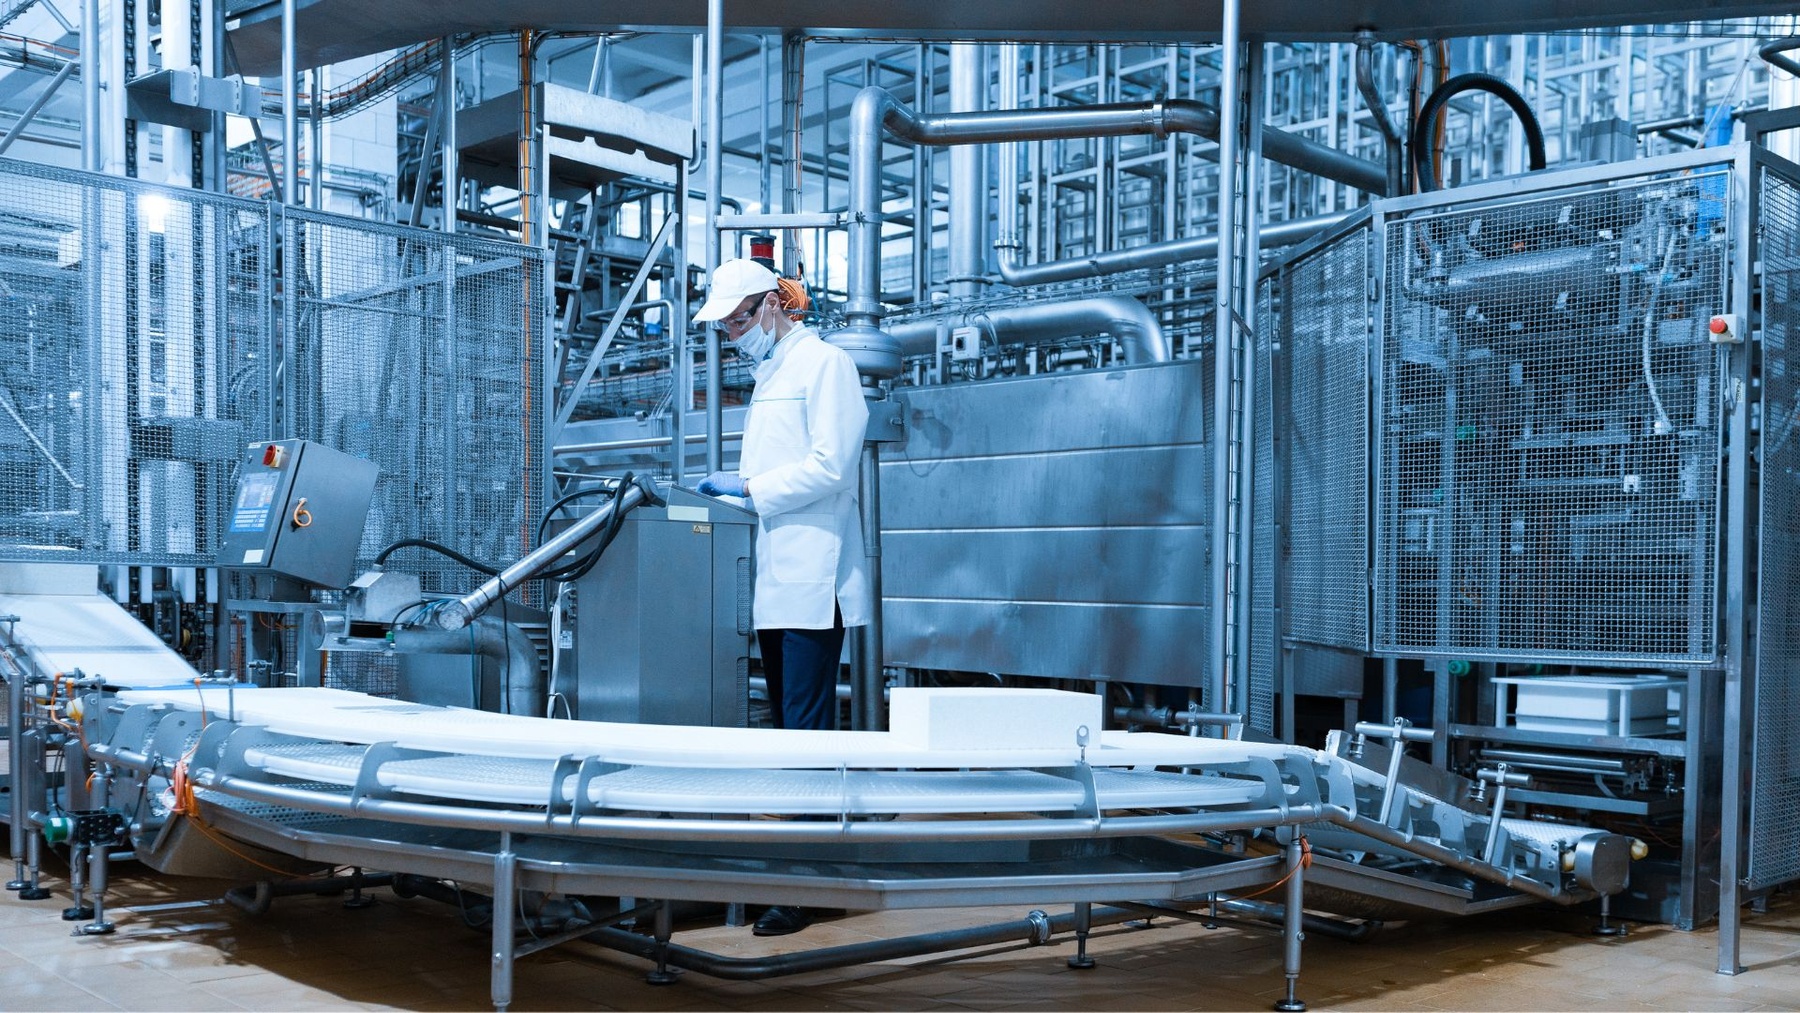
Our client, a premium chocolate and pastry manufacturer in Thailand, is looking for an experienced
Factory Manager to lead its manufacturing operations through the next stage of growth.
You’ll have full accountability for the factory, covering safety, quality, production, maintenance, supply chain and cost. You’ll take a hands-on approach to drive operational excellence: improving efficiency, cutting waste and manual work, strengthening planning, and building systems that can grow with the business.
A key part of the role is turning the team’s hands-on manufacturing know-how into standard processes, documented procedures and digital workflows. That way, the factory relies less on manual coordination and on what individual people know.
Job Responsibilities:1. Factory Operations Leadership
- Lead and manage the overall operations of the factory across chocolate and pastry manufacturing.
- Take full accountability for operational performance including safety, quality, output, efficiency, downtime, waste, and manufacturing cost.
- Ensure stable and disciplined factory operations through strong leadership, structure, and daily management routines.
- Build operational standards, workflows, KPIs, and management systems to support scalable growth.
- Drive operational ownership and accountability throughout all factory functions
2. Continuous Improvement & Operational Excellence
- Lead continuous improvement initiatives focused on productivity, labor efficiency, material yield, waste reduction, OEE improvement, and process optimization.
- Develop and implement lean manufacturing principles and operational excellence programs.
- Identify operational bottlenecks and implement sustainable corrective actions.
- Drive cost-conscious decision making throughout all manufacturing activities.
- Improve factory planning, line balancing, capacity utilization, and operational flow.
- Support automation and process improvement initiatives where commercially justified.
3. Systems, Planning & Digital Transformation
- Build and strengthen operational systems, standards, and workflows across all factory functions.
- Standardize processes to improve consistency, efficiency, traceability, and scalability.
- Capture and retain manufacturing know-how through SOPs, work instructions, process controls, and structured documentation.
- Reduce operational dependency on manual coordination and tribal knowledge.
- Improve production planning and cross-functional coordination between sales, supply chain, production, and logistics.
- Drive stronger use of data, KPIs, reporting systems, and digital tools to improve operational visibility and decision making.
- Support the development and implementation of ERP, planning, scheduling, and manufacturing management systems.
- Improve operational discipline through structured management routines, reporting cadence, and performance tracking.
- Identify opportunities for automation and digitalization that improve productivity, reduce errors, and support future business growth.
- Build sustainable systems that allow the factory to scale efficiently while maintaining quality and operational stability.
4. Supply Chain, Logistics & Inventory
- Lead SCM and logistics functions to ensure material availability and stable production flow.
- Improve inventory management, stock accuracy, warehouse efficiency, and logistics performance.
- Work closely with procurement and planning to optimize inventory levels and reduce operational risk.
- Drive improvements in inbound and outbound operational efficiency.
5. Maintenance & Engineering
- Oversee factory maintenance to ensure high equipment reliability and minimal downtime.
- Ensure preventive and predictive maintenance systems are implemented and sustained.
- Support equipment upgrades, factory improvements, and future expansion projects.
- Ensure proper management of utilities, infrastructure, and technical systems.
6. Health, Safety & Compliance
- Lead all health, safety, and environmental activities within the factory.
- Build and maintain a strong safety culture with clear accountability and operational discipline.
- Ensure compliance with food safety and regulatory standards including GMP, HACCP, FSSC 22000, and applicable Thai regulations.
- Ensure factory readiness for customer audits and certification requirements.
- Lead investigations and corrective actions related to operational or safety incidents.
7. Financial & Cost Management
- Manage factory operating costs and support achievement of company profitability targets.
- Monitor labor cost, manufacturing overhead, material losses, utilities, and operational spending.
- Identify and execute cost-saving initiatives without compromising safety or quality.
- Support budgeting, forecasting, and factory investment planning.
8. Leadership & Team Development
- Lead and develop cross-functional factory teams with strong performance management and accountability.
- Build organizational capability and succession planning within operations.
- Establish clear expectations, KPIs, and development plans for direct reports.
- Foster a culture of ownership, discipline, teamwork, and continuous improvement.
Required Qualifications:- Bachelor’s degree in Engineering, Food Science, Industrial Management, Manufacturing, or related field.
- Minimum 10 years of experience in food manufacturing operations.
- Minimum 5 years in a senior factory leadership or plant management role.
- Strong experience managing multi-department factory operations.
- Experience in chocolate, confectionery, bakery, pastry, or related food manufacturing environments strongly preferred.
- Strong understanding of food safety and manufacturing compliance standards.
- Proven experience driving operational efficiency and continuous improvement initiatives.
- Experience implementing or improving ERP, production planning, MES, or manufacturing management systems preferred.
- Strong capability in process mapping, workflow optimization, and operational system development.
- Experience improving organizational structure, accountability systems, and KPI-driven management.
- Proven ability to transition factories from highly manual operations into more structured and data-driven environments.